
Cable manufacturing is an important part of the electrical, energy, telecommunications, construction, automotive, and industrial infrastructure industries. Electrical cables and wires are used to transmit electrical power, distribute signals, connect equipment, and support communication networks across residential, commercial, and industrial environments.
The cable manufacturing industry involves several production stages, including conductor preparation, copper and aluminium wire drawing, stranding, insulation extrusion, shielding, armoring, and final testing. Different cable designs are developed according to voltage requirements, operating temperatures, mechanical strength, environmental conditions, and application-specific standards.
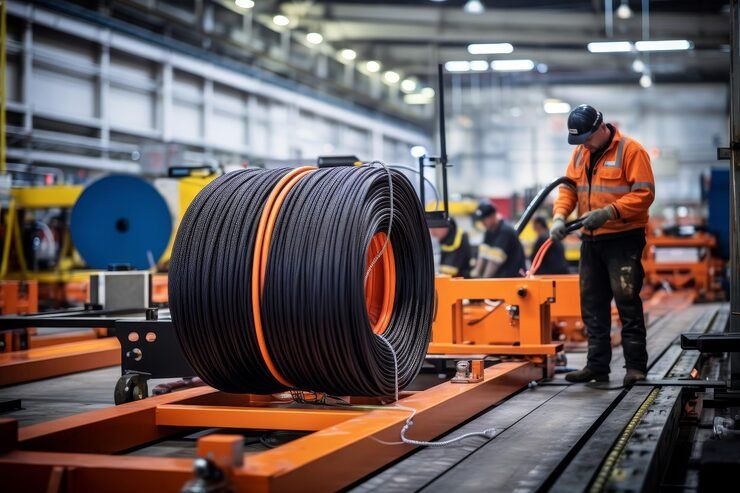
With the expansion of renewable energy, electric vehicles, industrial automation, data centers, and electrical infrastructure, demand for specialized cable technologies continues to develop. Understanding electrical cable types, raw materials, manufacturing processes, production machinery, and global manufacturers provides useful knowledge of this important industrial sector.
What Is Cable Manufacturing?
Cable manufacturing is the industrial process of producing electrical cables and wires by combining conductive materials with insulation, protective layers, and other components. The primary purpose of an electrical cable is to transmit electrical power or signals safely and reliably between different equipment, systems, and locations.
Copper and aluminium are the two major conductor materials used in electrical cable production. Copper is widely used because of its high electrical conductivity and mechanical properties, while aluminium is commonly selected for applications where lower conductor weight is important.
Depending on the intended application, manufacturers produce single-core cables, multicore cables, flexible cables, power cables, communication cables, control cables, and specialized industrial cables.
A finished cable may contain several layers, including the conductor, insulation, inner sheath, metallic screen, armor, and outer protective jacket. The construction depends on electrical requirements, installation conditions, and relevant technical standards.
Major Types of Electrical Cables
Electrical cables are classified according to conductor construction, insulation materials, voltage ratings, number of cores, and intended applications. Selecting the appropriate cable requires consideration of electrical load, installation environment, temperature, mechanical stress, and applicable safety standards.
Power Cables
Power cables are designed to transmit and distribute electrical energy between power generation facilities, substations, distribution networks, buildings, and industrial equipment.
They are manufactured in different voltage categories, including low-voltage, medium-voltage, and high-voltage configurations. Power cable construction may include copper or aluminium conductors, polymer insulation, metallic screening, and protective outer sheaths.
These cables are used in electrical distribution networks, manufacturing facilities, commercial buildings, infrastructure projects, and energy installations.
Low Voltage Cables
Low-voltage cables are commonly used in residential buildings, commercial properties, electrical panels, lighting systems, and industrial equipment.
They are generally designed for electrical systems operating up to 1,000 volts AC, subject to the relevant product classification and standard. Common insulation materials include PVC and XLPE.
Low-voltage cables are available in different conductor sizes, core configurations, and sheath materials according to installation requirements.
Medium Voltage Cables
Medium-voltage cables are used in electrical distribution systems connecting substations, transformers, industrial facilities, and large commercial installations.
Their construction generally includes a conductor, conductor screen, insulation, insulation screen, metallic screen, and protective outer sheath.
XLPE is commonly used as an insulation material because of its electrical and thermal properties. These cables require appropriate electrical testing and installation procedures.
High Voltage and Extra High Voltage Cables
High-voltage and extra-high-voltage cables are developed for electricity transmission over long distances and connections between major power infrastructure facilities.
These cables require specialized insulation systems, electrical field control, metallic screening, and carefully engineered accessories.
Depending on the application, manufacturers produce underground and submarine high-voltage cable systems for electricity transmission and interconnection projects.
Control Cables
Control cables are used to transmit control signals between electrical equipment, instruments, control panels, and automation systems.
They are commonly found in manufacturing plants, power stations, industrial machinery, and process control installations.
Control cables may include multiple insulated conductors, shielding, and protective jackets to support signal integrity and mechanical protection.
Instrumentation Cables
Instrumentation cables are designed to transmit measurement and monitoring signals between sensors, instruments, and control equipment.
They are widely used in chemical processing, oil and gas facilities, power plants, water treatment installations, and industrial automation systems.
Some instrumentation cable designs incorporate individual pair shielding, overall shielding, and insulation materials selected for the operating environment.
Flexible Electrical Cables
Flexible cables are designed for applications where movement, bending, or repeated positioning is required.
They are commonly used in portable equipment, industrial machinery, robotics, electrical appliances, and temporary power connections.
Their construction may include finely stranded copper conductors and flexible insulation and sheath materials.
Communication and Data Cables
Communication cables are used to transmit voice, data, and electronic signals across telecommunications and networking infrastructure.
Common categories include coaxial cables, Ethernet cables, twisted-pair cables, and fiber optic cables.
Fiber optic cables transmit information through optical fibers rather than conventional electrical conductors. They are important in high-speed telecommunications, internet infrastructure, data centers, and long-distance communication networks.
Copper and Aluminium Wire Production in Cable Manufacturing
Copper and aluminium are the primary conductive materials used in electrical cable production. Their electrical properties, mechanical characteristics, weight, and suitability for different installations influence cable design and manufacturing decisions.
Copper Wire Manufacturing Process
Copper wire manufacturing begins with copper rods, which are processed into smaller conductor wires through mechanical drawing operations. Copper is widely used in electrical applications because of its high electrical conductivity, ductility, and resistance to mechanical fatigue in suitable constructions.
The manufacturing process generally includes copper rod preparation, wire drawing, annealing, bunching or stranding, and quality inspection.
During wire drawing, copper rods pass through a series of precision dies that gradually reduce their diameter. Lubrication and controlled production conditions help maintain surface quality and dimensional accuracy.
Annealing is a heat treatment process used to restore ductility after mechanical drawing. It helps produce copper wires with the required flexibility and mechanical characteristics.
The processed copper wires are then combined through bunching or stranding to create conductors with the required cross-sectional area. These conductors are subsequently used in power cables, building wires, flexible cables, control cables, and specialized electrical products.
Aluminium Wire Manufacturing Process
Aluminium wire manufacturing follows a similar production sequence but involves material-specific process controls. Aluminium is valued for its relatively low density, making it useful in overhead transmission conductors and selected power distribution applications.
The process begins with aluminium rod preparation and wire drawing. The rod is passed through drawing dies to achieve the required wire diameter. Depending on the alloy and intended application, suitable heat treatment and mechanical processing may be applied.
After drawing, individual aluminium wires are stranded into conductors. Manufacturers may use different stranding arrangements to achieve the required electrical and mechanical characteristics.
Aluminium conductors are widely used in overhead power lines, distribution networks, underground power cables, and industrial electrical infrastructure.
Differences Between Copper and Aluminium Conductors
Copper and aluminium conductors have different characteristics that influence their selection in electrical systems.
Characteristic | Copper | Aluminium |
|---|---|---|
Electrical conductivity | Higher | Lower |
Density | Higher | Lower |
Weight | Heavier | Lighter |
Mechanical properties | Generally higher strength | Alloy and construction dependent |
Common applications | Building wiring, motors, industrial cables | Overhead transmission, power distribution |
Installation considerations | Connector compatibility and flexibility | Oxide management and compatible connectors |
The choice between copper and aluminium depends on current-carrying requirements, conductor dimensions, installation conditions, mechanical loading, connection design, and applicable electrical standards. Aluminium cables require suitable termination methods and connectors designed for the conductor material.
Electrical Cable Manufacturing Process: Step-by-Step Guide
Cable manufacturing involves several interconnected production operations. The exact sequence depends on the cable category, voltage rating, conductor material, insulation system, and intended application.
Raw Material Selection and Preparation
The manufacturing process begins with the selection of conductor materials, insulation compounds, shielding materials, armor components, and protective sheath materials.
Copper and aluminium rods are commonly used for conductor production. Polymer materials such as PVC, XLPE, polyethylene, and elastomer compounds are selected according to the cable's electrical and environmental requirements.
Manufacturers also procure metallic tapes, steel wires, fillers, water-blocking materials, and other components required for specialized cable construction.
Wire Drawing
Wire drawing reduces the diameter of copper or aluminium rods by pulling the material through progressively smaller dies.
This operation produces conductor wires with specified dimensions and surface characteristics. Drawing machines may use multiple dies, lubrication systems, cooling arrangements, and tension control equipment.
The required wire diameter depends on the final conductor size, strand configuration, and cable specification.
Annealing
Annealing is a controlled heat treatment process used to modify the mechanical properties of drawn metal wires.
During drawing, metal deformation can increase hardness and reduce ductility. Annealing helps restore flexibility and produces conductor wires suitable for subsequent stranding operations.
The temperature, duration, and atmosphere depend on the conductor material and manufacturing requirements.
Bunching and Conductor Stranding
Bunching and stranding combine multiple individual wires into a larger conductor assembly. These processes improve flexibility and allow manufacturers to produce conductors with different shapes and cross-sectional areas.
Common arrangements include concentric stranding, compact stranding, and sector-shaped conductor construction.
Stranding machines control wire tension, lay length, and conductor geometry. The resulting conductor is prepared for insulation and further cable assembly.
Insulation Extrusion
Insulation extrusion is one of the most important operations in electrical cable production. During this process, polymer compounds are heated and passed through an extrusion die to form a continuous insulating layer around the conductor.
Common insulation materials include:
PVC: Polyvinyl chloride is widely used in building wires and general-purpose electrical cables.
XLPE: Cross-linked polyethylene is used in many power cables because of its electrical and thermal properties.
PE: Polyethylene is used in selected power, communication, and data cable constructions.
EPR: Ethylene propylene rubber is used in flexible and specialized electrical cable applications.
LSZH: Low-smoke zero-halogen compounds are used in applications where smoke and corrosive gas characteristics are important considerations.
Extrusion equipment must maintain suitable temperature, pressure, material flow, and dimensional control to achieve consistent insulation thickness.
Screening and Shielding
Certain power, control, and instrumentation cables require screening or shielding to manage electrical stress or reduce electromagnetic interference.
High-voltage power cables may incorporate semiconductive conductor and insulation screens to control the electric field around the conductor.
Control and instrumentation cables may use metallic foil, copper braid, or other shielding arrangements to protect signal transmission from external interference.
Cabling and Core Assembly
Multicore cables are manufactured by combining multiple insulated conductors into a single cable assembly.
Cabling machines arrange the cores in a specified configuration. Fillers, binding tapes, and other materials may be added to maintain the required shape and construction.
The assembly process must maintain the specified core arrangement and avoid unnecessary mechanical stress on the insulated conductors.
Inner Sheathing and Bedding
An inner sheath or bedding layer may be applied around the assembled cable cores. It provides a supporting layer between the insulated conductors and the outer protective components.
Depending on the design, manufacturers may use polymer extrusion, wrapping tapes, or other suitable materials.
Cable Armoring
Armoring provides additional mechanical protection for cables installed in environments where impact, compression, or external mechanical damage may occur.
Common armor materials include galvanized steel wire, steel tape, and aluminium wire. The appropriate arrangement depends on the cable construction, installation environment, and electrical design requirements.
Outer Sheathing and Cable Jacketing
The outer sheath is the final protective layer applied to many electrical cables. It helps protect the internal cable components against moisture, abrasion, chemicals, sunlight, and other environmental conditions.
PVC, polyethylene, LSZH compounds, and specialized polymer materials may be used depending on the intended application.
Final Inspection and Packaging
After manufacturing, finished cables undergo inspection and testing according to the relevant product standards and specifications.
Testing may include conductor resistance measurement, insulation resistance, high-voltage testing, dimensional inspection, and mechanical testing.
Once the required inspections are completed, cables are marked, measured, coiled or wound onto drums, sealed, and prepared for transportation.
The manufacturing sequence and testing requirements differ across cable categories.
Major Machinery Used in Cable Manufacturing Plants
Cable manufacturing facilities use specialized machinery to process conductors, apply insulation, assemble cable cores, and complete protective layers. Production line configurations depend on factory capacity, cable specifications, and product categories.
Wire Drawing Machines
Wire drawing machines reduce the diameter of copper and aluminium rods through precision dies. They may include single-wire drawing systems, multi-wire drawing machines, intermediate drawing machines, and fine-wire drawing equipment.
Important operating considerations include drawing speed, die condition, lubrication, wire tension, cooling, and dimensional accuracy.
Annealing Machines
Annealing machines use controlled heating systems to improve conductor flexibility and achieve specified mechanical properties.
Depending on the production setup, manufacturers may use inline resistance annealing systems or separate heat treatment equipment.
Stranding and Bunching Machines
Stranding and bunching machines combine individual metal wires into conductors with specific configurations.
Common equipment includes rigid stranding machines, tubular stranding machines, planetary stranding machines, and double-twist bunching machines.
Cable Extrusion Machines
Cable extrusion machines apply insulation and protective polymer layers around electrical conductors.
A typical extrusion line may contain a pay-off system, preheater, extruder, crosshead die, cooling trough, diameter measurement system, spark tester, capstan, and take-up equipment.
Multilayer extrusion systems can apply different polymer layers during a coordinated production operation.
Cabling and Laying-Up Machines
Cabling machines combine insulated cores into multicore cable constructions. Their configurations depend on cable diameter, core count, required lay length, and production speed.
Armoring Machines
Armoring machines apply metallic protective layers around cable assemblies. Depending on the product design, they may use steel wire, steel tape, or aluminium wire.
Cable Testing and Inspection Equipment
Quality laboratories use electrical and mechanical testing instruments to assess finished cable performance. Common equipment includes high-voltage testers, insulation resistance meters, conductor resistance measurement systems, spark testers, tensile testing machines, and dimensional measurement instruments.
Modern production facilities may also integrate online inspection systems and automated process monitoring.
Advanced Cable Manufacturing Technologies
Advances in materials science, extrusion engineering, production automation, and electrical infrastructure are influencing modern cable manufacturing. Manufacturers are developing specialized products to support renewable energy, electric mobility, high-voltage transmission, telecommunications, and industrial automation.
XLPE Insulation Technology
Cross-linked polyethylene (XLPE) is widely used in power cable manufacturing because of its electrical insulation properties, thermal performance, and suitability for different voltage applications.
XLPE insulation is produced through a controlled manufacturing process in which polyethylene is cross-linked to create a network structure. The process improves its thermal and mechanical characteristics compared with conventional thermoplastic polyethylene.
XLPE cables are used in low-voltage, medium-voltage, and high-voltage electrical distribution and transmission systems.
High Voltage Cable Manufacturing Technology
High-voltage cable production requires specialized conductor designs, insulation systems, semiconductive screens, metallic sheaths, and protective layers.
Manufacturing facilities may use triple extrusion technology to apply conductor screening, XLPE insulation, and insulation screening in a coordinated process.
These cables are used in underground transmission networks, electrical substations, offshore wind projects, and large power infrastructure installations.
Submarine and Underwater Cable Technology
Submarine power cables are designed to transmit electrical energy across underwater routes connecting islands, offshore energy facilities, and mainland electricity networks.
Their construction may include specialized insulation, metallic barriers, water-blocking components, armor, and external protection.
Submarine cable manufacturing requires strict control over material selection, mechanical construction, electrical testing, and installation-related specifications.
Solar and Photovoltaic Cable Technology
Solar cables are designed for photovoltaic installations connecting solar panels, junction boxes, inverters, and other electrical components.
These cables generally require suitable resistance to ultraviolet radiation, temperature variations, moisture, and environmental exposure.
Photovoltaic cable manufacturing uses specialized insulation and sheath compounds selected according to the relevant electrical and environmental standards.
Electric Vehicle Charging Cable Technology
Electric vehicle charging cables connect charging equipment with electric vehicles and are designed for electrical safety, mechanical flexibility, and repeated handling.
Their construction may include flexible copper conductors, specialized insulation, protective jackets, shielding, and additional components depending on the charging system.
The expansion of electric vehicle infrastructure is creating demand for charging cables and associated electrical connection technologies.
Fire-Resistant and Low-Smoke Cable Technology
Fire-resistant cables are designed to maintain specified electrical circuit functions for defined periods under particular fire test conditions.
Low-smoke and zero-halogen cable compounds are used in selected buildings, transportation systems, public infrastructure, and industrial facilities where smoke density and corrosive gas emissions are important considerations.
These cable designs must meet the applicable fire performance and material testing requirements.
Fiber Optic Cable Manufacturing Technology
Fiber optic cables transmit information using light signals through optical fibers. They are widely used in telecommunications, broadband networks, data centers, and industrial communication infrastructure.
Their manufacturing involves optical fiber preparation, fiber coating, buffering, strength member integration, cable assembly, and protective jacketing.
Specialized constructions may include loose-tube, tight-buffered, ribbon, and armored fiber optic cables.
Quality Control and Testing in Cable Manufacturing
Quality control is essential in cable manufacturing because electrical performance, insulation integrity, mechanical strength, and environmental resistance influence the reliability of finished products.
Manufacturers establish inspection procedures throughout the production process, from incoming raw materials to final cable testing.
Conductor Resistance Testing
Conductor resistance testing measures the electrical resistance of copper or aluminium conductors.
The results help verify whether the conductor meets the specified electrical requirements. Measurements are generally evaluated with reference to conductor dimensions, material properties, and temperature conditions.
Insulation Resistance Testing
Insulation resistance testing evaluates the electrical resistance of the insulation system between conductors or between a conductor and an appropriate reference point.
It helps identify certain insulation defects and assess insulation performance under specified testing conditions.
High Voltage Testing
High-voltage testing evaluates the electrical withstand characteristics of cable insulation under prescribed test conditions.
Depending on the cable category and applicable standard, manufacturers may perform routine, sample, or type tests.
Partial Discharge Testing
Partial discharge testing is particularly important for certain medium-voltage and high-voltage cable systems.
It helps identify localized electrical discharge activity within insulation or at interfaces under specified electrical conditions. This testing supports the assessment of insulation quality and manufacturing consistency.
Dimensional and Physical Testing
Physical inspections may include conductor diameter, insulation thickness, outer sheath thickness, cable diameter, conductor construction, and marking verification.
Mechanical testing may evaluate tensile strength, elongation, flexibility, and other characteristics relevant to the specified cable design.
Flame and Environmental Testing
Depending on the intended application, cable testing may include flame propagation, smoke emission, halogen content, water penetration, ultraviolet exposure, chemical resistance, and temperature performance.
The appropriate testing program depends on cable type, applicable standards, and customer specifications.
International Standards and Certifications for Electrical Cables
Electrical cables are manufactured according to technical standards that establish requirements for conductor construction, insulation materials, electrical performance, mechanical properties, testing, and product identification.
IEC Standards
The International Electrotechnical Commission develops international standards for electrical and electronic technologies.
IEC standards are widely referenced in power cable design, manufacturing, testing, and installation. Different publications cover low-voltage cables, medium-voltage cables, high-voltage systems, and specialized cable categories.
ISO Quality Management Standards
The International Organization for Standardization publishes standards used by organizations to establish and maintain quality management systems.
ISO 9001 is commonly used by manufacturing organizations to structure quality management processes, documentation, process monitoring, and continual improvement.
Certification to a management system standard does not automatically establish that every manufactured cable meets every applicable product specification.
UL Standards
In North America, UL Solutions provides testing and certification programs for various electrical products and cable categories.
Applicable UL requirements depend on the cable's intended use, construction, and market.
National and Regional Electrical Standards
Cable manufacturers may also follow national and regional requirements such as applicable BIS standards in India, BS standards in the United Kingdom, and other market-specific electrical and product regulations.
Buyers and engineering teams should verify the exact standard, edition, certification scope, and product approval applicable to their installation.
Global Cable Manufacturers and Industrial Suppliers
The global cable industry includes companies producing building wires, power cables, transmission systems, industrial cables, fiber optic products, and specialized electrical conductors.
The following are examples of established manufacturers operating in relevant cable markets.
Prysmian Group
Prysmian Group develops cable systems for energy transmission, power distribution, telecommunications, and industrial applications.
Its product areas include low-voltage, medium-voltage, high-voltage, submarine, and fiber optic cable technologies. The company also participates in major electrical infrastructure and energy transmission projects.
Nexans
Nexans manufactures cable products and systems for buildings, infrastructure, industrial markets, and energy transmission.
Its product portfolio includes power cables, renewable energy cables, submarine systems, telecommunications cables, and specialized industrial cable solutions.
Southwire
Southwire produces electrical wire, building cables, power distribution products, industrial cables, and related electrical equipment.
Its product categories include bare copper conductors, aluminium overhead conductors, low-voltage cables, medium-voltage cables, mining cables, and instrumentation cables.
NKT
NKT specializes in power cable systems for electricity transmission and distribution.
Its product and project activities include low-voltage, medium-voltage, high-voltage, and submarine cable systems used in electricity infrastructure and renewable energy projects.
Sumitomo Electric Industries
Sumitomo Electric Industries operates across electrical components, energy infrastructure, telecommunications, and industrial technologies.
Its cable-related activities include power cables, communication systems, automotive wiring, and specialized electrical products.
LS Cable & System
LS Cable & System develops power cable systems, submarine cables, telecommunications cables, and industrial electrical products.
Its technologies are relevant to energy infrastructure, industrial facilities, and international power transmission projects.
KEI Industries
KEI Industries manufactures a range of electrical wires and cables for residential, commercial, industrial, and infrastructure applications.
Its product categories include low-voltage, medium-voltage, and high-voltage cables, as well as specialized electrical cable products.
Polycab India
Polycab India operates in the electrical wire and cable industry, with products serving building infrastructure, industrial facilities, and power distribution applications.
Havells India
Havells India manufactures electrical products, including building wires and cables, for residential, commercial, and industrial markets.
When evaluating cable manufacturers or industrial cable suppliers, purchasers should examine product specifications, conductor material, voltage ratings, insulation systems, manufacturing capabilities, applicable certifications, testing documentation, and technical support.
A manufacturer's general product portfolio should not be treated as confirmation that every product is suitable for a particular electrical installation.
Industrial Applications of Electrical Cable Manufacturing
Electrical cables support a wide range of industries by connecting power sources, electrical equipment, control systems, communication infrastructure, and automation technologies.
Power Generation and Electricity Distribution
Power cables are used in power plants, substations, transformers, and electrical distribution networks.
They connect generators, switchgear, transformers, and distribution equipment. High-voltage cable systems are also used in underground transmission and interconnection infrastructure.
Renewable Energy and Solar Power Plants
Renewable energy projects require specialized electrical cables for connecting photovoltaic modules, inverters, transformers, wind turbines, and electrical grid infrastructure.
Solar cable systems are used in photovoltaic installations, while wind power projects require cables for turbine connections, internal distribution networks, and offshore energy transmission.
Oil and Gas Industry
Oil and gas facilities use power, control, instrumentation, and communication cables in processing plants, refineries, drilling facilities, and pipeline infrastructure.
Cable construction must account for operating temperature, mechanical stress, chemical exposure, and hazardous-area requirements where applicable.
Construction and Building Infrastructure
Electrical wires and cables are essential in residential buildings, commercial complexes, hospitals, educational institutions, airports, and industrial buildings.
They support lighting, electrical distribution, HVAC systems, elevators, security systems, fire protection systems, and building automation.
Automotive and Electric Vehicle Manufacturing
Automotive manufacturing uses electrical wiring harnesses, battery cables, sensor cables, control wiring, and communication systems.
Electric vehicles require specialized high-voltage cables for battery connections, electric motors, power electronics, and charging systems.
Industrial Automation and Manufacturing
Manufacturing facilities use control cables, motor cables, sensor cables, instrumentation cables, and industrial communication cables.
These products connect PLC systems, industrial robots, motors, sensors, drives, and automated production machinery.
Telecommunications and Data Centers
Fiber optic cables, Ethernet cables, and other communication cables support internet connectivity, data transmission, network infrastructure, and digital communication systems.
Data centers use specialized power and communication cable systems to connect servers, networking equipment, cooling systems, and electrical distribution infrastructure.
Mining and Heavy Industries
Mining operations require specialized cables for underground equipment, mobile machinery, conveyor systems, pumps, and electrical distribution.
These cables may require additional mechanical protection, flexibility, abrasion resistance, and environmental suitability.
Cable Manufacturing Industry: Market Developments and Emerging Opportunities
The cable manufacturing industry is closely connected to electricity demand, infrastructure development, industrial expansion, telecommunications, and renewable energy projects. Changes in these sectors influence the development of new cable materials, production technologies, and specialized electrical products.
Renewable Energy Cable Demand
Solar farms, offshore wind projects, and other renewable energy installations require specialized cable systems for power generation and transmission.
The expansion of renewable energy infrastructure is increasing the importance of photovoltaic cables, medium-voltage cables, high-voltage transmission systems, and submarine power cables.
Electric Vehicle Charging Infrastructure
The development of electric mobility is creating additional requirements for high-voltage automotive cables, battery connection cables, charging cables, and charging station electrical infrastructure.
Cable manufacturers are developing products with suitable thermal performance, flexibility, insulation properties, and electrical safety characteristics.
Smart Manufacturing and Automated Cable Production
Modern cable factories are incorporating industrial automation, programmable logic controllers, digital monitoring, and automated inspection systems.
These technologies help manufacturers monitor production parameters, manage equipment performance, reduce material wastage, and maintain consistent manufacturing conditions.
High-Speed Data and Telecommunications Infrastructure
Increasing demand for cloud computing, broadband connectivity, artificial intelligence infrastructure, and data centers is supporting the development of fiber optic cables and specialized communication products.
Manufacturers are also developing higher-capacity optical cable designs and specialized connectivity systems for telecommunications networks.
Advanced Insulation and Sustainable Materials
Research into polymer compounds, insulation technologies, and recyclable materials is influencing cable manufacturing.
Manufacturers are examining improved material formulations, low-smoke compounds, halogen-free materials, and production processes designed to reduce environmental impact.
Factors to Consider When Selecting Electrical Cable Manufacturers and Suppliers
Selecting an appropriate cable manufacturer requires technical evaluation rather than relying only on product descriptions or company reputation.
Cable Specifications and Electrical Requirements
Buyers should identify the required conductor material, cross-sectional area, voltage rating, number of cores, insulation type, and operating temperature.
The cable must be appropriate for the electrical load and intended installation conditions.
Manufacturing Capabilities
Manufacturers should be evaluated according to their production capabilities, machinery, extrusion technologies, conductor processing facilities, and ability to manufacture specialized cable constructions.
For projects involving high-voltage or submarine cables, specialized production facilities and engineering capabilities are particularly important.
Quality Testing and Certifications
Buyers should examine applicable product standards, test reports, certification documents, and quality management procedures.
Relevant documentation may include conductor resistance results, insulation testing, mechanical testing, and other assessments specified for the cable category.
Raw Material Quality
The quality of copper, aluminium, insulation compounds, shielding materials, and protective sheaths influences cable performance.
Material traceability and incoming inspection procedures are important considerations when evaluating manufacturing operations.
Technical Documentation and Product Support
Cable manufacturers should provide relevant technical documentation, including product datasheets, conductor specifications, installation guidance, and applicable testing information.
For specialized industrial projects, engineering documentation and compatibility with electrical equipment are also important.
Future of Cable Manufacturing Technologies
The future of cable manufacturing will be influenced by developments in energy infrastructure, electric transportation, industrial automation, and digital communication.
High-voltage direct current transmission systems are receiving attention for long-distance electricity transmission and offshore renewable energy connections. Advanced insulation systems and submarine cable engineering will remain important areas of development.
Automation and digital manufacturing technologies are also expected to influence production efficiency. Real-time monitoring, automated dimensional inspection, predictive maintenance, and digital production records can help manufacturers manage complex manufacturing operations.
In addition, demand for electric vehicles, charging infrastructure, smart grids, and data centers is creating requirements for specialized cable products. Manufacturers will continue to evaluate conductor designs, insulation materials, shielding systems, and protective constructions to meet these evolving applications.
Conclusion
Cable manufacturing is an essential industrial activity supporting electrical infrastructure, power transmission, renewable energy, construction, telecommunications, automotive production, and industrial automation.
The industry involves several specialized processes, including copper and aluminium wire drawing, annealing, conductor stranding, insulation extrusion, screening, cabling, armoring, and protective sheathing. Each stage contributes to the electrical, mechanical, and environmental characteristics of the finished cable.
Technologies such as XLPE insulation, high-voltage cable engineering, submarine power cables, solar cables, EV charging cables, and fiber optic systems are expanding the range of applications for modern cable products.
For manufacturers, engineering teams, and industrial purchasers, understanding cable specifications, production machinery, quality testing, international standards, and supplier capabilities is important when evaluating electrical cable systems. As global infrastructure and energy requirements continue to evolve, cable manufacturing will remain an important part of modern industrial development.