Twin-screw extruder machines are industrial processing systems designed to transport, mix, melt, and shape materials through the coordinated movement of two rotating screws inside a barrel.
They are widely used in plastic manufacturing, polymer compounding, chemical processing, food production, and selected pharmaceutical applications.
The machine typically receives raw materials through a hopper or feeding system. As the two screws rotate, they move the material through heated sections of the barrel. Depending on the material and machine configuration, the process may include blending, melting, dispersing additives, removing moisture, and developing the pressure needed to push the material through a die.
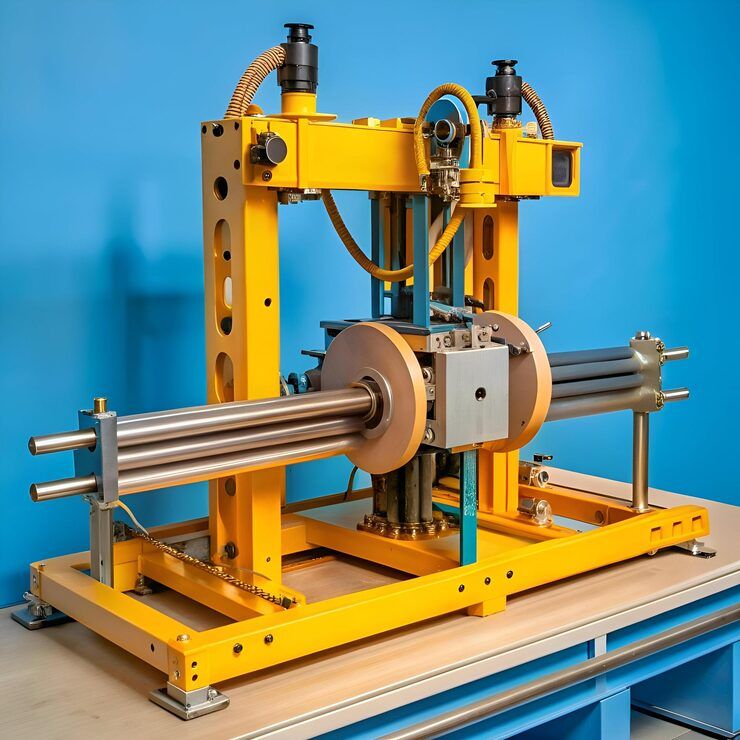
A die is an opening that gives the processed material its initial shape as it leaves the machine. The output may be plastic strands, pellets, profiles, or another continuous form. Additional equipment can cool, cut, shape, or collect the material after extrusion.
Twin-screw extruders differ from single-screw machines because they use two screws rather than one. This arrangement can provide greater flexibility in mixing and material handling, particularly when a formulation contains several ingredients. However, the actual performance depends on screw geometry, rotation direction, temperature, torque, feed rate, and material properties.
These machines are available in laboratory, pilot-scale, and industrial configurations. Smaller systems help engineers test formulations, while larger installations support continuous manufacturing. Understanding the working principles of twin-screw extrusion helps explain its role in producing consistent materials for modern industrial applications.
Importance of Twin-Screw Extruder Machines
Twin-screw extruders are important because they combine several processing functions within one system. Their configuration can be adjusted for different materials, making them useful in manufacturing processes that require controlled mixing and consistent output.
Plastic Compounding and Polymer Blending
Plastic compounding involves combining a base polymer with other ingredients to produce a material with particular characteristics. Additives may influence colour, stiffness, impact resistance, flame resistance, flexibility, or resistance to environmental conditions.
A twin-screw extruder can distribute pigments, mineral fillers, stabilisers, and reinforcing fibres throughout a polymer mixture. For example, coloured plastic pellets can be produced by blending a polymer with pigments and other additives before the material is cooled and cut into pellets.
The quality of the compound depends on ingredient compatibility, feeding accuracy, temperature control, and the amount of mixing applied during processing.
Processing Recycled Plastics
Twin-screw extruders are used in selected recycling processes to blend recovered plastics with compatible polymers or additives. The objective may be to produce recycled compounds with more consistent processing characteristics or to prepare material for another manufacturing stage.
Recycled plastics can contain variations in colour, moisture, contamination, and molecular structure. Sorting, cleaning, drying, and filtration may therefore be necessary before extrusion. The machine alone cannot eliminate every contaminant or restore all properties lost through previous use.
Continuous Industrial Production
Extrusion is a continuous process when raw material enters the machine steadily and processed material exits at a controlled rate. This arrangement can support integration with feeders, cooling systems, pelletisers, conveyors, and packaging equipment.
Stable operation depends on maintaining suitable material flow, temperature, screw speed, and downstream handling. Poor coordination between these stages may cause blockages, irregular output, or product defects.
Processing Complex Formulations
Some industrial formulations contain ingredients with different particle sizes, melting behaviour, or flow characteristics. Twin-screw machines can use different screw elements and barrel sections to manage conveying, mixing, melting, and venting.
Special feeding systems can introduce powders, liquids, or fibres at specific points. Venting sections may remove moisture or volatile compounds where appropriate. These features make the equipment adaptable to a range of formulations, although each process requires suitable engineering and testing.
Types of Twin-Screw Extruder Machines
Twin-screw extruders are classified according to screw rotation, the relationship between the screws, and their intended application. These characteristics influence how the material moves and how effectively the machine performs different processing tasks.
Co-Rotating Twin-Screw Extruders
In co-rotating extruders, both screws rotate in the same direction. Many industrial models use intermeshing screws, allowing material to move through the spaces formed by the screw flights and barrel.
Co-rotating systems are widely used for polymer compounding because their screw elements can be arranged to support conveying, melting, dispersing, and mixing. They are commonly applied in colour masterbatch production, filled plastics, engineering polymers, and selected recycled-material formulations.
Counter-Rotating Twin-Screw Extruders
Counter-rotating extruders have two screws that rotate in opposite directions. Depending on the design, the screws may be intermeshing or non-intermeshing.
These machines are commonly associated with particular profile-extrusion applications, including rigid polyvinyl chloride (PVC) processing. Their material-conveying characteristics can suit formulations that require controlled flow and pressure development.
The choice between co-rotating and counter-rotating designs depends on the polymer, desired output, product geometry, and processing requirements.
Intermeshing and Non-Intermeshing Extruders
Intermeshing screws engage closely with one another, allowing material to pass through a controlled space between the screw flights. This arrangement can support effective mixing and material transfer.
Non-intermeshing screws have a different spatial relationship, with their flights operating without the same close engagement. Their mixing and conveying behaviour depends on the particular design.
Intermeshing describes the physical relationship between the screws, whereas co-rotating and counter-rotating describe their direction of rotation. These are separate classification features.
Laboratory, Pilot-Scale, and Industrial Extruders
Twin-screw extruders are also available in different sizes for development and manufacturing.
- Laboratory extruders: Used to investigate formulations and processing conditions with small material quantities.
- Pilot-scale extruders: Used to evaluate processes before transferring them to larger equipment.
- Industrial extruders: Designed for sustained production and integration with automated material-handling systems.
Moving from a laboratory machine to a larger system requires careful evaluation. Changes in heat transfer, residence time, torque, screw geometry, and material flow can affect the results.
How Twin-Screw Extruder Machines Work
The extrusion process involves several stages, each of which influences the properties and consistency of the final material.
Feeding and Material Conveying
Raw materials enter the machine through a hopper or a controlled feeding system. Feeders regulate the amount of polymer and additives supplied to the screws.
When a formulation contains several ingredients, separate feeders may introduce them in measured proportions. Accurate feeding helps maintain the intended composition and reduces variations between batches or production periods.
Heating and Melting
The rotating screws move the material through the barrel while external heaters raise its temperature. Mechanical energy from the screws also contributes to heating.
For thermoplastics, the combined effects soften or melt the polymer. The temperature profile must suit the specific material because excessive heat can cause degradation, discolouration, or changes in mechanical properties.
Different barrel sections may operate at different temperatures to support feeding, melting, mixing, and discharge.
Mixing and Compounding
As the material moves through the screws, it experiences repeated movement and deformation. Specialised screw elements can increase mixing, disperse additives, or help distribute reinforcing materials throughout the polymer.
The required mixing intensity depends on the formulation. Too little mixing may leave unevenly distributed ingredients, while excessive mechanical energy can damage sensitive materials or generate unwanted heat.
Some machines include venting sections to remove moisture or volatile compounds. These sections must be configured carefully to avoid excessive material loss.
Extrusion, Cooling, and Pelletising
After processing, the material passes through a die. In polymer compounding, the output often emerges as strands that are cooled and cut into small pellets.
Other systems use different dies and downstream equipment to produce profiles, sheets, or specialised shapes. Cooling and cutting conditions must match the material's behaviour and the required dimensions.
Finished material may then undergo inspection to check appearance, size, moisture content, or other relevant characteristics.
Developments in twin-screw extrusion increasingly focus on process monitoring, recycled-material processing, formulation control, and improved energy management. The practical results depend on the machine configuration and the materials being processed.
Automation and Digital Monitoring
Modern extrusion lines can use sensors and programmable controls to monitor barrel temperatures, screw speed, pressure, motor load, and feed rates. Operators can use these measurements to identify process changes and investigate possible causes of inconsistent output.
Some systems also analyse operating data to support predictive maintenance. For example, an unusual change in motor load may indicate a feed problem, material variation, or mechanical issue. Such monitoring supports decision-making but does not eliminate the need for inspection and trained operators.
Recycled Polymer Processing
Recycling remains an important application area for extrusion technology. Twin-screw systems can blend selected recycled polymers with compatible additives or other materials to produce compounds for particular applications.
Processing recycled material requires attention to contamination, moisture, degradation, and changes in polymer composition. Better sorting and feed preparation can improve consistency, but the suitability of recycled material must be verified through testing.
Energy and Temperature Management
Extrusion equipment uses energy for heating, screw rotation, cooling, and associated material-handling operations. Improvements in heater control, drive systems, insulation, and screw design may help reduce unnecessary energy use.
The total energy requirement depends on the entire production line, including material drying, feeding, cooling, and pelletising. A machine's performance should therefore be assessed under realistic operating conditions rather than by considering one component alone.
Advanced Polymer Formulations
Twin-screw extrusion supports the development of engineering plastics, fibre-reinforced polymers, polymer blends, and compounds containing specialised additives. Research also continues into materials designed for particular thermal, mechanical, electrical, or environmental properties.
These formulations may require careful control of temperature, shear, residence time, and ingredient distribution. Laboratory trials and material testing remain important before transferring a formulation to industrial production.
Laws or Policies Related to Twin-Screw Extruder Machines in India
Twin-screw extruder operations in India may be affected by environmental rules, plastic-waste requirements, factory safety provisions, and standards for particular finished products. The applicable requirements depend on the manufacturing activity and materials involved.
Plastic Waste Management Rules
The Plastic Waste Management Rules, 2016, and subsequent amendments establish a framework for plastic-waste management in India. Depending on their role, businesses may need to consider waste handling, registration, reporting, or Extended Producer Responsibility (EPR) requirements.
A company using a twin-screw extruder is not automatically subject to every EPR obligation. Its responsibilities depend on whether it manufactures plastic packaging, recycles plastic waste, produces covered products, or undertakes another regulated activity.
The Central Pollution Control Board (CPCB) provides official information through its and Operators should consult current notifications and guidance before determining their obligations.
Environmental Permissions
Industrial facilities may require consent or other approvals from the relevant State Pollution Control Board or Pollution Control Committee. Requirements depend on location, industrial classification, emissions, waste generation, and the type of manufacturing activity.
Facilities handling recycled plastics should establish appropriate arrangements for segregating materials, managing contaminants, and disposing of process waste. Environmental controls should be based on the actual materials and production methods used.
Workplace and Machine Safety
Twin-screw extruders contain rotating machinery, heated surfaces, electrical systems, and pressurised processing sections. Suitable guarding, emergency-stop mechanisms, maintenance procedures, and operator training are important for reducing workplace hazards.
Factories must identify and comply with applicable occupational safety and factory legislation, including relevant provisions of the Occupational Safety, Health and Working Conditions Code, 2020, and associated rules as brought into force. Current requirements should be verified for the particular establishment and location.
Product-Specific Standards
Finished products may be subject to additional requirements based on their intended use. For example, plastics used in food-contact applications must meet applicable food-safety and packaging requirements. Components intended for medical, electrical, or automotive applications may have further material and performance specifications.
Manufacturers should maintain appropriate material records, process documentation, and quality-inspection results where required.
Tools and Resources for Twin-Screw Extruder Machines
Technical resources help engineers select equipment, develop formulations, monitor operating conditions, and maintain consistent output.
Machine Manuals and Screw Configuration Guides
Machine manuals describe operating limits, screw assembly, barrel settings, startup procedures, shutdown methods, and maintenance requirements. Screw configuration guides explain how different elements support conveying, kneading, and mixing.
These documents should match the machine model and intended process. Incorrect assembly or unsuitable settings can affect product quality and create safety risks.
Material Data Sheets
Material data sheets provide information about polymer properties, recommended processing temperatures, moisture sensitivity, and chemical compatibility. They help engineers determine whether a material is appropriate for the intended extrusion process.
Recycled materials and complex blends may vary between batches, so laboratory testing may be needed in addition to supplier documentation.
Process Monitoring Instruments
Common instruments include temperature sensors, pressure transducers, screw-speed indicators, motor-load monitors, and gravimetric feeders. These devices help operators identify process variations and investigate possible faults.
Laboratory testing may measure melt-flow behaviour, tensile strength, moisture content, or other properties relevant to the finished product.
Computer-Aided Engineering Software
Engineering software can assist with screw design, die geometry, material flow, and heat-transfer analysis. Simulation may help identify potential pressure variations or areas where mixing needs adjustment.
However, results depend on the accuracy of material data and modelling assumptions. Physical trials and product testing remain necessary to validate a new formulation or machine configuration.
Comparison of Key Machine Selection Factors
| Factor | Purpose |
|---|---|
| Screw diameter | Influences machine dimensions and processing capacity |
| Length-to-diameter ratio | Determines the available processing length |
| Torque capacity | Defines the mechanical load the drive can handle |
| Temperature zones | Support controlled heating along the barrel |
| Screw configuration | Influences conveying, mixing, and material distribution |
| Feeding system | Regulates the supply of polymers and additives |
| Venting arrangement | Helps remove moisture or volatile compounds where needed |
| Downstream equipment | Supports cooling, cutting, pelletising, or shaping |
Frequently Asked Questions About Twin-Screw Extruder Machines
What are twin-screw extruder machines used for?
Twin-screw extruder machines transport, melt, mix, and process materials continuously. Common applications include plastic compounding, colour masterbatch production, recycled-plastic processing, food extrusion, and selected pharmaceutical manufacturing processes.
What is the difference between co-rotating and counter-rotating extruders?
Co-rotating extruders have screws that rotate in the same direction, while counter-rotating machines have screws that rotate in opposite directions. The different arrangements affect material flow, mixing behaviour, and the applications for which each machine is suitable.
Which materials can twin-screw extruders process?
Depending on their configuration, these machines can process thermoplastic polymers, polymer blends, pigments, fillers, reinforcing fibres, and selected food or pharmaceutical formulations. Material compatibility must be assessed against the machine's temperature, torque, feeding, and processing capabilities.
How do twin-screw extruders improve material mixing?
The two screws move and deform material repeatedly as it travels through the barrel. Specialised screw elements can support different mixing functions and help distribute ingredients throughout a formulation. The outcome depends on screw geometry, temperature, rotation speed, feed rate, and material properties.
What maintenance do twin-screw extruder machines require?
Maintenance may include inspecting screws and barrels for wear, checking heaters and sensors, examining the drive system, cleaning feeding components, and testing safety devices. The schedule should follow the manufacturer's instructions and reflect the operating conditions and materials used.
Conclusion
Twin-screw extruder machines are widely used in plastics manufacturing, polymer compounding, recycling, and other continuous-processing industries. Their two-screw arrangement provides flexibility for transporting, melting, mixing, and processing complex formulations. Automation, process monitoring, material recovery, and improved temperature management continue to shape the technology. Understanding machine types, material properties, operating conditions, and applicable Indian regulations helps manufacturers select and operate extrusion systems appropriately.